
 |


17-4PH (UNS S17400, Grade 630, DIN 1.4542) is a martensitic precipitation-hardening stainless steel that reaches its final properties through a single low-temperature ageing treatment. This page gives the full chemistry, every standard H-condition mechanical property, heat treatment schedule, corrosion and temperature limits, sour-service rules and the exact information your purchase order must carry.
Common names | 17-4PH, UNS S17400, Grade 630, AISI/SUS 630, DIN 1.4542, EN X5CrNiCuNb16-4, ISC S51740 |
Structure | Martensitic precipitation-hardening (age-hardening) stainless steel |
Supplied condition | Solution-annealed Condition A; final properties set by ageing at 482 to 621 °C |
Strength range | Yield 517 MPa at H1150-M up to 1170 MPa at H900 - a spread of more than 2x from one chemistry |
Hardness range | 28 HRC (H1150-M) to 47 HRC (H900); Condition A capped at 38 HRC and 363 HB |
Continuous service limit | About 316 °C (600 °F); avoid long holds in 370 to 480 °C |
Corrosion level | Comparable to Type 304 in most environments; clearly below 316 in chlorides |
Sour service | NACE MR0175 compliance depends on measured hardness, not on the H-code name |
Magnetic response | Ferromagnetic in every condition - unlike 304, 316 and duplex austenitics |
Must appear on the order | Grade, standard plus edition, product form, H-condition and hardness requirement |
17-4PH is not one material. It is one chemistry delivered in nine standard heat-treated conditions, and the difference between the strongest and the softest is more than double the yield strength - 1170 MPa at H900 against 517 MPa at H1150-M. Specifying the grade without the condition is the single most common and most expensive mistake buyers make on this alloy.
Alloy 17-4PH (UNS S17400), also written as Grade 630 or SUS 630, is a chromium-nickel-copper precipitation-hardening martensitic stainless steel with an addition of niobium. It is supplied in the solution-annealed Condition A and reaches its final properties through one low-temperature ageing treatment at 482 to 621 °C, which precipitates copper-rich phases in the martensitic matrix. 17-4PH combines high strength and hardness with corrosion resistance broadly comparable to Type 304 stainless steel, which is why it is used wherever a part needs the strength of a heat-treated alloy steel together with the corrosion behaviour of a stainless.
Key point: because the ageing temperature sets every mechanical value, the heat-treatment condition belongs on the purchase order line, not in a footnote. A line that reads simply "17-4PH" is not a complete specification.
17-4PH is a chromium-nickel-copper stainless steel that is hardened by a low-temperature ageing step rather than by a quench, because dissolved copper precipitates out as fine particles that block dislocation movement. The name reads as its chemistry: about 17 % chromium, about 4 % nickel, and PH for precipitation hardening.
The mechanism is worth understanding because it explains every number further down this page. After solution annealing the alloy is a relatively soft, low-carbon martensite with copper held in supersaturated solution. Holding it at 482 to 621 °C lets copper atoms diffuse into tiny coherent precipitates. These precipitates pin dislocations, so the steel gets stronger and harder without the distortion and cracking risk that a conventional high-carbon quench-and-temper cycle would bring. Age it hotter or longer and the precipitates coarsen, which trades strength for toughness and ductility - and that is exactly what the H-code ladder is.
Because the carbon content is low (0.07 % maximum), 17-4PH is not prone to the quench cracking of conventional martensitic grades, and the ageing treatment runs at such a low temperature that scaling and distortion stay small. That combination - heat treat after machining, with minimal movement - is why the alloy dominates precision parts such as valve stems, fasteners, pump shafts and aircraft fittings. See aerospace applications and oil and gas applications for where it is used in practice.
17-4PH is nominally 15.0 to 17.5 % chromium, 3.0 to 5.0 % nickel and 3.0 to 5.0 % copper, with 0.15 to 0.45 % niobium plus tantalum and a maximum of 0.07 % carbon. Copper is the hardening element and niobium controls grain size and helps tie up carbon.
Chemical composition of Alloy 17-4PH (reproduced unchanged)
Grade | C≤ | Si≤ | Mn≤ | P≤ | S≤ | Cr | Ni | Cu | Nb+Ta |
17-4PH | 0.07 | 1 | 1 | 0.04 | 0.03 | 15-17.5 | 3-5 | 3-5 | 0.15-0.45 |
Density is 7.75 g/cm³, the elastic modulus is about 196 GPa, and thermal conductivity sits near 18 W/m·K at 100 °C - roughly a quarter of carbon steel, which is why heat builds up at the cutting edge and why welding distortion needs managing.
Typical physical properties of 17-4PH (mill data-sheet values, not specification minimums)
Property | Value | Why it matters |
Density | 0.280 lb/in³, 7.75 g/cm³ | Weight take-off and shipping estimates |
Specific heat | 0.11 BTU/lb.°F at 70 °F, 460 J/kg.°C at 20 °C | Heat-up and cool-down transients |
Melting range | 2560 to 2625 °F, 1404 to 1440 °C | Welding and hot-forming windows |
Elastic modulus, tension | About 196 GPa (28.5 × 10^6 psi) | Deflection and stiffness calculations |
Thermal conductivity at 100 °C | About 18 W/m·K | Machining heat and welding distortion |
Mean coefficient of thermal expansion, 20 to 100 °C | About 10.8 um/m.°C | Clearances and fit over temperature |
Magnetic response | Ferromagnetic in all conditions | Disqualifies it where non-magnetic parts are required |
The same alloy appears as UNS S17400, ASTM Type 630, JIS SUS 630, DIN 1.4542, EN X5CrNiCuNb16-4, ISO X5CrNiCuNb 16-4 and GB 0Cr17Ni4Cu4Nb. They describe the same chemistry; they do not guarantee the same mechanical limits, so always name the governing standard alongside the grade.
17-4PH international equivalent grades (reproduced unchanged)
| SAE | JIS | NF | DIN | UNS | GB | ASTM | ISO | KS | EN | ISC |
|---|---|---|---|---|---|---|---|---|---|---|
| 17-4PH | SUS 630 | Z6CNU17-04 | 1.4542 | S17400 | 0Cr17Ni4Cu4Nb | 630 | X5CrNiCuNb 16-4 | STS 630 | X5CrNiCuNb 16-4 | S51740 |
Ultimate tensile strength runs from 1310 MPa at H900 down to 862 MPa at H1150-M, and yield strength drops even faster, from 1170 MPa to about 517 MPa. This is the table to design against, because any single set of numbers quoted for "17-4PH" describes one specific condition and not the alloy.
The values below are specification minimums for longitudinal test pieces in bar form per ASTM A564/A564M Type 630 and AMS 5643. Two honest caveats belong next to any such table. First, mills routinely produce values five to ten percent above these minimums, and typical mill figures answer a different question: use minimums for design allowables and acceptance, typicals only for machining and cost estimates, and never mix the two in one calculation. Second, product form and section size matter - a large forging will not reach the same numbers as a small bar in the same condition.
17-4PH minimum mechanical properties by condition (ASTM A564/A564M Type 630, AMS 5643)
Condition | Tensile strength min, MPa (ksi) | Yield strength 0.2 % min, MPa (ksi) | Elongation min, % | Typical hardness |
A (solution annealed) | not specified as a minimum; typical about 1030 (149) | not specified as a minimum; typical about 760 (110) | - | 363 HB max (38 HRC max) |
H900 | 1310 (190) | 1170 (170) | 10 | 40 to 47 HRC |
H925 | 1170 (170) | 1070 (155) | 10 | 38 to 45 HRC |
H1025 | 1070 (155) | 1000 (145) | 12 | 34 to 42 HRC |
H1075 | 1000 (145) | 862 (125) | 13 | 31 to 38 HRC |
H1100 | 965 (140) | 793 (115) | 14 | 29 to 36 HRC |
H1150 | 931 (135) | 724 (105) | 16 | 28 to 37 HRC |
H1150-D (double aged) | 860 (125) | 725 (105) | 16 | 24 to 33 HRC |
H1150-M (overaged) | 862 (125) | 517 (75) | 18 | 255 HB max |
Data note. The single-row mechanical summary previously published on this page listed a tensile strength of 23.3 ksi (160 MPa), a yield strength of 16.68 ksi (115 MPa), 5 % elongation and 217 HBW. Those values cannot be reconciled with any condition of ASTM A564 Type 630, every one of which specifies a tensile strength of at least 931 MPa and a yield strength of at least 517 MPa. The original row is retained below unchanged for traceability. Use the condition-by-condition table above for design, specification and acceptance testing.
Original single-row mechanical summary as previously published
Grade | Tensile, min,ksi[MPa] | Yield, 0.02%offset, min, ksi[MPa] | Elongation, %(min) | Hardness |
17-4PH | 23.3[160] | 16.68[115] | 5 | 217HBW |
Read the ladder as a trade rather than a ranking. Going from H900 to H1150 costs you about 30 % of the tensile strength and buys roughly a tripling of impact energy, a large gain in ductility, and a substantial improvement in resistance to stress corrosion cracking. No condition is "the best"; the right answer is set by which of those four properties actually governs your part.
Condition A is produced by solution treating at 1038 ± 14°C for half an hour and cooling below 32°C, which completes the martensite transformation. Ageing then sets the final properties. Anything that has been hot worked, forged or cast has to be solution annealed again first, or it will not respond correctly to ageing.
| Condition | Treatment | Temperature | Hold | Cooling |
|---|---|---|---|---|
| A | Solution anneal | 1038 ± 14°C | 0.5 h | Oil, water+polymer or air to <32°C |
| H900 | Age | 482 ± 9°C | 1 h | Air |
| H925 | Age | 496°C | 4 h | Air |
| H1025 | Age | 552°C | 4 h | Air |
| H1075 | Age | 579°C | 4 h | Air |
| H1100 | Age | 593°C | 4 h | Air |
| H1150 | Age | 621°C | 4 h | Air |
| H1150-D | Double age | 621°C + 621°C | 4 h + 4 h | Air / air |
| H1150-M | Condition + age | 760°C then 621°C | 2 h + 4 h | Air / air |
| Two rules that cause most shop problems. Material has to be cooled to at least 32°C before ageing, because the martensite finish temperature sits near 32°C and ageing warm material leaves low ductility. And material ordered to AMS 5643 is aged in a tighter window, 482 ± 6°C for 1 hour ± 5 minutes, which is not the same as commercial ASTM A564 practice. |
17-4PH stainless steel has many material standards, such as AMS 5604, ASTM A693, ASTM A564, etc. These standards specify the 17-4PH chemical composition, mechanical properties, heat treatment methods, etc. The following are the material standards for stainless steel 17-4PH tubes, plates, forgings, round bars, wires, and rings:
Product | Standard | Show |
17-4PH Customized Forging | AMS 5643 |  |
17-4PH Stainless Steel Bars | AMS 5643 |  |
17-4PH Stainless Steel Plates/Sheets/Strips | AMS 5604 |  |
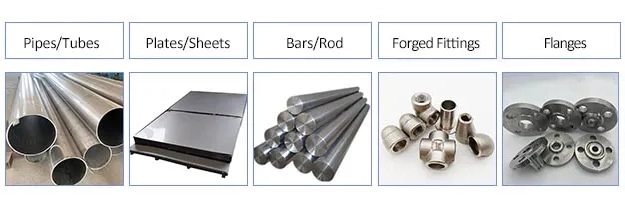
JN Alloy supplies this grade as bar, plate, sheet, strip and forgings. Browse round bars, stainless steel round bars, stainless steel sheet and plate and alloy pipe for the full product range.
Solution anneal at 1038 plus or minus 14 °C for half an hour and cool below 32 °C to complete the martensite transformation, then age at the temperature that maps to the condition you specified - 482 °C for H900 through 621 °C for H1150.
Solution annealing and ageing codes for 17-4PH (reproduced unchanged)
Condition | Treatment | Temperature | Hold | Cooling |
A | Solution anneal | 1038 ± 14°C | 0.5 h | Oil, water+polymer or air to <32°C |
H900 | Age | 482 ± 9°C | 1 h | Air |
H925 | Age | 496°C | 4 h | Air |
H1025 | Age | 552°C | 4 h | Air |
H1075 | Age | 579°C | 4 h | Air |
H1100 | Age | 593°C | 4 h | Air |
H1150 | Age | 621°C | 4 h | Air |
H1150-D | Double age | 621°C + 621°C | 4 h + 4 h | Air / air |
H1150-M | Condition + age | 760°C then 621°C | 2 h + 4 h | Air / air |
Two rules cause most shop problems. Material has to be cooled to at least 32 °C before ageing, because the martensite finish temperature sits near 32 °C and ageing warm material leaves low ductility. And material ordered to AMS 5643 is aged in a tighter window than commercial ASTM A564 practice, which is not the same tolerance band - so state the standard on the order, not just the H-code. Anything that has been hot worked, forged or cast must be solution annealed again first, or it will not respond correctly to ageing.
17-4PH in H900 is roughly five and a half times stronger than 316 in yield strength - 1170 MPa against 205 MPa - and still about 2.6 times stronger than duplex 2205. That is the entire reason to specify it, and it comes with a corrosion trade you should accept deliberately.
This comparison is the one most often left out of technical pages, and it is the question engineers actually arrive with. On pure strength nothing in the common stainless family comes close. But note the second half of the table: 17-4PH gives up chloride pitting resistance to get that strength, because it carries no molybdenum and sits at a PREN of roughly 16 to 17, below the threshold normally required for seawater service.
Strength and hardness comparison at room temperature
Grade | Structure | Tensile min, MPa | Yield 0.2 % min, MPa | Elongation min, % | Typical hardness | Magnetic? |
17-4PH H900 | Martensitic PH | 1310 | 1170 | 10 | 40 to 47 HRC | Yes |
17-4PH H1150 | Martensitic PH | 931 | 724 | 16 | 28 to 37 HRC | Yes |
304 | Austenitic | 515 | 205 | 40 | 201 HB max | No, annealed |
316 | Austenitic | 515 | 205 | 40 | 217 HB max | No, annealed |
Duplex 2205 | Ferritic-austenitic | 620 | 450 | 25 | 293 HB max | Yes |
Super duplex 2507 | Ferritic-austenitic | 800 | 550 | 15 | 310 HB max | Yes |
Choose deliberately between the two directions. If the design is strength-limited, 17-4PH wins by a wide margin. If it is corrosion-limited in chlorides, step sideways to duplex or super duplex stainless steel, and if it is both strength- and chloride-limited, the honest answer is usually a nickel alloy rather than a stainless of any family - see the Hastelloy C276 guide for where that boundary falls. Note also that 17-4PH is ferromagnetic in every condition, which disqualifies it outright where a non-magnetic part is required.
In most environments the corrosion resistance of 17-4PH is comparable to Type 304 and clearly better than the 400 series martensitic grades, but it is measurably below 316 in chloride service. Its calculated PREN is only about 16 to 17, which puts seawater immersion out of bounds.
The comparison to 304 is the standard benchmark and it holds for atmospheric exposure, many process chemicals, and food, dairy, paper and petroleum service, where 17-4PH is often reported as comparable to 304L. It is superior to the straight-chromium 400 series because of its higher chromium level together with nickel and copper. But it carries no molybdenum, so in chlorides it cannot match 316, and it will suffer crevice corrosion and pitting when exposed to stagnant seawater over time.
Three corrosion behaviours deserve special attention because the heat treatment controls them. First, Condition A should generally not be placed in service: it is subject to brittle fracture and is more sensitive to chloride stress corrosion cracking than aged material. Second, where chloride stress corrosion cracking is a risk, select a higher ageing temperature - 550 °C is the commonly recommended tempering temperature for chloride service and about 590 °C is preferred in H2S media. Third, ageing above roughly 495 °C increases sensitisation susceptibility through grain-boundary chromium carbide precipitation, so highly corrosive service at the top of the H-code range calls for a double-aged condition rather than a simple H-code.
Corrosion resistance of 17-4PH by environment
Environment | Performance | Guidance |
Atmospheric, rural and industrial | Good, comparable to 304 | No restriction |
Fresh water, steam condensate | Good | Routine choice |
Food, dairy, pulp and paper, petroleum | Comparable to 304L | Widely used |
Marine atmosphere, intermittent immersion | Fair | Acceptable; avoid stagnant conditions |
Seawater immersion or crevices | Poor - pitting and crevice attack | Use duplex, super duplex or a nickel alloy instead |
Chloride stress corrosion cracking risk | Condition dependent | Age at 550 °C or above; never use Condition A |
Sour service, H2S bearing | Conditional | See the NACE section below |
Treat 316 °C as the conservative continuous service ceiling, and avoid prolonged exposure between 370 and 480 °C entirely, because that band precipitates a chromium-rich alpha-prime phase that embrittles the alloy and permanently destroys room-temperature toughness.
The limit is set by two different mechanisms and it helps to separate them. The first is simple over-ageing: because the alloy is aged at 482 to 621 °C during manufacture, any service temperature approaching those values will continue the ageing process, coarsening the copper precipitates and progressively softening the part. Strength falls steadily as the service temperature climbs toward 400 °C.
The second mechanism is embrittlement rather than softening. Long holds in roughly 370 to 480 °C precipitate the alpha-prime phase - the classic 475 °C embrittlement - and above about 540 °C sigma phase can form. Both cost room-temperature impact toughness, and neither can be reversed by re-heat treatment without a full re-solution anneal.
Temperature bands for 17-4PH service
Metal temperature | Verdict | Reason |
Down to about minus 73 °C | Acceptable in the tougher conditions | H1100 and H1150 retain usable toughness; check Charpy for the condition supplied |
Up to 316 °C continuous | Recommended operating band | Properties remain stable with no significant over-ageing risk |
316 to 370 °C | Caution, short term only | Strength begins to drift; limit cumulative exposure |
370 to 480 °C long holds | Avoid | Alpha-prime embrittlement removes room-temperature toughness |
Above 540 °C long holds | Avoid | Sigma phase formation in addition to continued over-ageing |
Above roughly 600 °C | Use a different alloy | Consider A286 to about 700 °C or Inconel 718 to about 650 °C |
Short excursions are not the same as service. The Feature list on this grade quotes strength to 600 °F, creep-rupture strength to 900 °F and oxidation resistance to about 1100 °F - those describe capability and intermittent exposure, not a continuous design limit. Design the continuous case to about 316 °C and treat anything higher as a requalification exercise.
Yes, but only in the overaged conditions and only when the measured hardness is at or below the ceiling the project specification sets - commonly 33 HRC for 17-4PH. NACE MR0175 and ISO 15156-3 set hardness limits; they do not simply approve an H-code, so a condition name alone never proves compliance.
Sour service means the produced fluid contains hydrogen sulfide at a partial pressure above 0.05 psi, roughly 0.3 kPa, which creates a risk of sulfide stress cracking at stresses far below yield. Susceptibility correlates directly with hardness, which is why the standard controls hardness rather than naming treatments.
In practice that puts the conditions on a clear spectrum: H900 at 40 HRC minimum is disqualified outright, H1025 at 35 HRC minimum exceeds the ceiling on paper and would need heat-specific verification, and the overaged conditions are the only defensible choices.
17-4PH conditions and sour-service fitness (screening guide only)
Condition | Specified hardness | Fitness for sour service | What to require |
H900 | 40 to 47 HRC | Not suitable | Do not specify where H2S is present |
H925 | 38 to 45 HRC | Not suitable | Exceeds the common 33 HRC ceiling |
H1025 | 34 to 42 HRC | Not suitable without proof | Minimum exceeds the ceiling; only with documented actual hardness at or below the limit |
H1075 | 31 to 38 HRC | Marginal | Heat-specific hardness verification required |
H1100 | 29 to 36 HRC | Borderline | Borderline; verify every heat |
H1150 | 28 to 37 HRC | Commonly accepted | Require measured hardness at or below the ceiling on the certificate |
H1150-D | 24 to 33 HRC | Recommended | Double aged; verify and record |
H1150-M | 255 HB max | Recommended for severe H2S | Maximum toughness and lowest hardness |
Screening only. This table is a first-pass guide built from the hardness ranges the specifications publish, not a substitute for engineering review against the current edition of NACE MR0175 / ISO 15156-3. Final acceptance always requires a qualified materials engineer, and in severe sour service 100 % hardness verification with the results recorded on the material test report.
Weld it in the solution-annealed Condition A with a matching ER630 filler, then age the whole fabrication, because welding in the aged condition leaves a softened heat-affected zone that cannot be recovered without a full re-solution anneal. Most standard processes work: SMAW, GTAW, PAW and GMAW.
The metallurgy dictates the sequence. If you weld an already-aged part, the heat-affected zone sees temperatures above its original ageing temperature and locally over-age, so the joint region ends up weaker than the parent metal. The only way to restore full strength is a complete re-solution anneal followed by a repeat of the ageing cycle - a furnace operation that is impractical for most assemblies. So the standard shop route is to weld in Condition A, then age the finished fabrication, which develops uniform properties everywhere.
Welding 17-4PH: process and filler guidance
Situation | Recommended approach | Reason |
Standard fabrication, can be heat treated after welding | Weld in Condition A with matching ER630 filler, then solution anneal and age the assembly | Gives uniform aged properties across parent metal, HAZ and weld |
Repair or addition where post-weld heat treatment is impossible | Accept reduced HAZ strength, or use an austenitic filler for crack resistance | An austenitic weld metal is more forgiving but will not match the parent strength |
Joining 17-4PH to carbon or low-alloy steel | Use an austenitic buffer filler appropriate to the dissimilar joint | Manages dilution across the transition |
High restraint or thick section | Control heat input and interpass temperature, and consider a pre-qualified procedure | Martensitic structures need controlled thermal cycles |
Confirm filler selection and qualification against AWS A5.9 and the applicable AMS or ASTM procedure specification for your product form. For general welding discipline on high-alloy materials, the approaches set out in the Hastelloy C276 welding guide carry over directly.
Machine it in the soft Condition A and age afterwards, because ageing is the lowest-distortion hardening route available and it removes the need to cut material at 40 HRC. The dimensional change on ageing is small and predictable - under 0.0005 in/in for H900 and less for the higher-temperature conditions.
17-4PH can be machined in both the solution-treated and the precipitation-hardened conditions, but the economics are very different. Machining characteristics vary with hardness: high-speed steel tools are acceptable and carbide is preferred, with standard lubrication. Fully aged H900 material behaves more like a tool steel than a stainless at the cutting edge, demanding lower speeds, more frequent tool changes and rigid setups.
This is why most fabricators rough-machine or fully machine in Condition A, then age, allowing for the known shrinkage on critical dimensions.
· Machine in Condition A wherever tolerances allow; age to the required H-code afterwards.
· Allow for predictable shrinkage on ageing - typically under 0.0005 in/in at H900, less at higher ageing temperatures.
· Use carbide tooling and standard lubrication; high-speed steel is acceptable but slower.
· Account for dimensional change caused by heat treatment if very stringent tolerances are required.
· Avoid thermal cutting such as plasma; prefer bandsaw, abrasive waterjet, shearing and machining.
Forming follows its own rules. Hot forming is done uniformly at 950 to 1200 °C, and must be followed by a full solution anneal, cooling below 25 °C, and ageing at the required temperature - the post-forming heat treatment is a function of the desired properties.
Cold forming is limited: it can only be undertaken on plates in the fully annealed condition, and stress corrosion resistance is enhanced by re-ageing at the precipitation hardening temperature after cold working.
17-4PH is selected wherever high strength, moderate corrosion resistance and dimensional stability have to coexist. Its established application areas include aerospace structural parts, biomedical hand tools, chemical processing, food process equipment, general mechanical components, nuclear waste processing and storage, oil and gas production including foils and helicopter deck platforms, and pulp and paper mill equipment.
· Aerospace - structural parts and fittings. See aerospace applications.
· Oil and gas - valve stems, wellhead components, fasteners and shafts. See oil and gas applications.
· Biomedical - hand tools and instruments.
· Chemical processing - see chemical equipment.
· Marine hardware and splash-zone components - see marine engineering; note that immersion service requires a different alloy.
· Food process equipment, mechanical components, nuclear waste storage, and pulp and paper mill equipment.
· 17-4PH is one chemistry in nine conditions. Always specify the H-code, never the grade alone.
· Yield strength ranges from 1170 MPa at H900 to 517 MPa at H1150-M - more than a factor of two.
· Hardness is the cheapest reliable proxy for condition on receipt and the decisive number for sour-service compliance.
· Continuous service is limited to about 316 °C, and long holds between 370 and 480 °C must be avoided.
· Corrosion resistance is comparable to 304 in most media, clearly below 316 in chlorides, and PREN is only about 16 to 17.
· For sour service specify H1150-D or H1150-M with measured hardness at or below the project ceiling.
· Machine in Condition A, then age - it is faster, cheaper and more dimensionally predictable than cutting aged material.
· 17-4PH is ferromagnetic, so it is ruled out wherever a non-magnetic part is required.
· 304 stainless steel - the corrosion benchmark 17-4PH is measured against.
· 316 stainless steel - the molybdenum-bearing comparison.
· 304 vs 316 stainless steel - properties and applications.
· Duplex 2205 - the step up in chloride resistance.
· Duplex and super duplex stainless steel.
· Duplex 2205 vs super duplex 2507.
· 904L vs 254 SMO vs 316L - super-austenitic options.
· Ultimate guide to Hastelloy C276 - when no stainless will do.
· Inconel 718 - high strength retained to about 650 °C.
· Round bars and stainless steel round bars.
· Stainless steel sheet and plate.
Q1. What is 17-4PH stainless steel?
17-4PH, also known as UNS S17400, Type 630 or DIN 1.4542, is a martensitic precipitation-hardening stainless steel containing about 17 percent chromium, 4 percent nickel, 3 to 5 percent copper and 0.15 to 0.45 percent niobium plus tantalum. It is hardened by a single low-temperature ageing treatment rather than by quenching.
Q2. What does the H in H900 mean?
The H stands for the ageing treatment and the number is the ageing temperature in degrees Fahrenheit. H900 means aged at 900 °F, which is 482 °C. Higher numbers mean a hotter ageing treatment, which produces lower strength but higher toughness and better stress corrosion cracking resistance.
Q3. What is the strongest condition of 17-4PH?
H900 is the strongest standard condition, with a minimum tensile strength of 1310 MPa (190 ksi) and a minimum yield strength of 1170 MPa (170 ksi) at 40 to 47 HRC. It has the lowest toughness of the standard conditions and is unsuitable for sour service.
Q4. What is the difference between Condition A and the H conditions?
Condition A is the solution-annealed starting state supplied so that parts can be machined before hardening. It is relatively soft and no standard intends it for service. The H conditions are the aged, ready-for-service states with specified mechanical properties.
Q5. Is 17-4PH magnetic?
Yes. 17-4PH is ferromagnetic in every condition because it has a martensitic structure. This distinguishes it from austenitic grades such as 304 and 316, and rules it out wherever a non-magnetic component is required.
Q6. What is the yield strength of 17-4PH?
It depends entirely on the condition. Minimum yield strength is 1170 MPa at H900, 1000 MPa at H1025, 793 MPa at H1100, 724 MPa at H1150 and about 517 MPa at H1150-M. There is no single yield strength for the grade.
Q7. What is the hardness of 17-4PH?
Typical hardness ranges from 28 HRC in H1150-M up to 47 HRC in H900. Condition A is capped at 38 HRC and 363 HB. Always state the scale and range you require on the purchase order.
Q8. How strong is 17-4PH compared with 316 stainless steel?
At H900 the yield strength of 17-4PH is 1170 MPa against 205 MPa for 316, roughly 5.7 times higher. The trade-off is corrosion: 316 carries molybdenum and resists chlorides far better, while 17-4PH has a PREN of only about 16 to 17.
Q9. Can 17-4PH be welded?
Yes, by most standard processes including SMAW, GTAW, PAW and GMAW. The preferred route is to weld in Condition A with a matching filler and then age the whole fabrication, because welding already-aged material softens the heat-affected zone.
Q10. What filler metal is used for welding 17-4PH?
A matching ER630 filler is the standard choice when the assembly can be heat treated after welding. Where post-weld heat treatment is impossible, an austenitic filler gives better crack resistance but will not match the parent metal strength. Confirm against AWS A5.9 and your qualified welding procedure.
Q11. Is 17-4PH corrosion resistant?
Its corrosion resistance is comparable to Type 304 stainless steel in most environments and superior to the 400 series martensitic grades. It is clearly below 316 in chloride service, and it suffers pitting and crevice attack in stagnant seawater.
Q12. What is the maximum service temperature of 17-4PH?
About 316 °C (600 °F) for continuous service. Prolonged exposure between 370 and 480 °C must be avoided because of alpha-prime embrittlement, and long holds above about 540 °C risk sigma phase formation.
Q13. Why should 17-4PH not be used between 370 and 480 °C?
Holding the alloy in that band precipitates a chromium-rich alpha-prime phase, the classic 475 °C embrittlement, which sharply reduces room-temperature impact toughness. The damage cannot be reversed without a full re-solution anneal.
Q14. Is 17-4PH suitable for sour service under NACE MR0175?
Only in the overaged conditions and only when the measured hardness meets the project ceiling, commonly 33 HRC. H1150, H1150-D and H1150-M are the defensible choices, while H900 at 40 HRC minimum is disqualified. NACE MR0175 sets hardness limits rather than approving condition names.
Q15. Which 17-4PH condition should I choose for a valve stem in sour service?
Specify H1150-D or H1150-M with hardness verified at or below the project ceiling and recorded on the material test report. H1150-M gives the highest toughness and lowest hardness for the most severe H2S duty.
Q16. What standards cover 17-4PH?
ASTM A564 and A705 cover bars, wire and shapes; ASTM A693 covers plate, sheet and strip; AMS 5643 covers aerospace bar and forgings; AMS 5604 covers aerospace flat products; and ASTM A747 covers the cast equivalent CB7Cu-1.
Q17. What is the difference between ASTM A564 and AMS 5643?
AMS 5643 is the aerospace specification and applies tighter control over chemistry, properties and testing than the commercial ASTM A564. Even for identically named conditions the minimums and test frequency can differ, so always cite the standard and revision together with the condition.
Q18. How machinable is 17-4PH?
Machinability depends strongly on hardness. The usual route is to machine in the soft Condition A and then age, which is faster, cheaper and more dimensionally predictable. Machining fully aged H900 demands carbide tools, lower speeds and rigid setups because the material behaves like a tool steel at the cutting edge.
Q19. Does 17-4PH change size during heat treatment?
Yes, slightly. Ageing causes a small predictable shrinkage, typically under 0.0005 in/in for H900 and less for the higher-temperature conditions. Allow for it on critical dimensions and machine to final size with that movement in mind.
Q20. Can 17-4PH be cold formed?
Only to a limited extent. Cold forming can generally be done on plates in the fully annealed condition only, and stress corrosion resistance is improved by re-ageing at the precipitation hardening temperature after cold working.
Q21. How do I identify 17-4PH on receipt?
Use positive material identification by XRF and look for copper at 3 to 5 percent together with niobium plus tantalum at 0.15 to 0.45 percent. Then hardness test to confirm the condition, and read the material test report for the standard, edition and heat treatment record.
Q22. What is the density of 17-4PH?
The density is 0.280 lb/in³, which is 7.75 g/cm³. Other typical physical values are an elastic modulus of about 196 GPa, a melting range of 1404 to 1440 °C and a mean coefficient of thermal expansion of about 10.8 um/m.°C between 20 and 100 °C.
Q23. What are the equivalent grades of 17-4PH?
UNS S17400, ASTM Type 630, JIS SUS 630, KS STS 630, DIN 1.4542, EN X5CrNiCuNb 16-4, ISO X5CrNiCuNb 16-4, NF Z6CNU17-04, GB 0Cr17Ni4Cu4Nb and ISC S51740 all describe the same alloy.
Q24. What applications is 17-4PH used for?
Aerospace structural parts, biomedical hand tools, chemical processing equipment, food process equipment, general mechanical components, nuclear waste processing and storage, oil and gas production components such as valve stems and fasteners, and pulp and paper mill equipment.


